
SP3 automatic drum and IBC filling machine
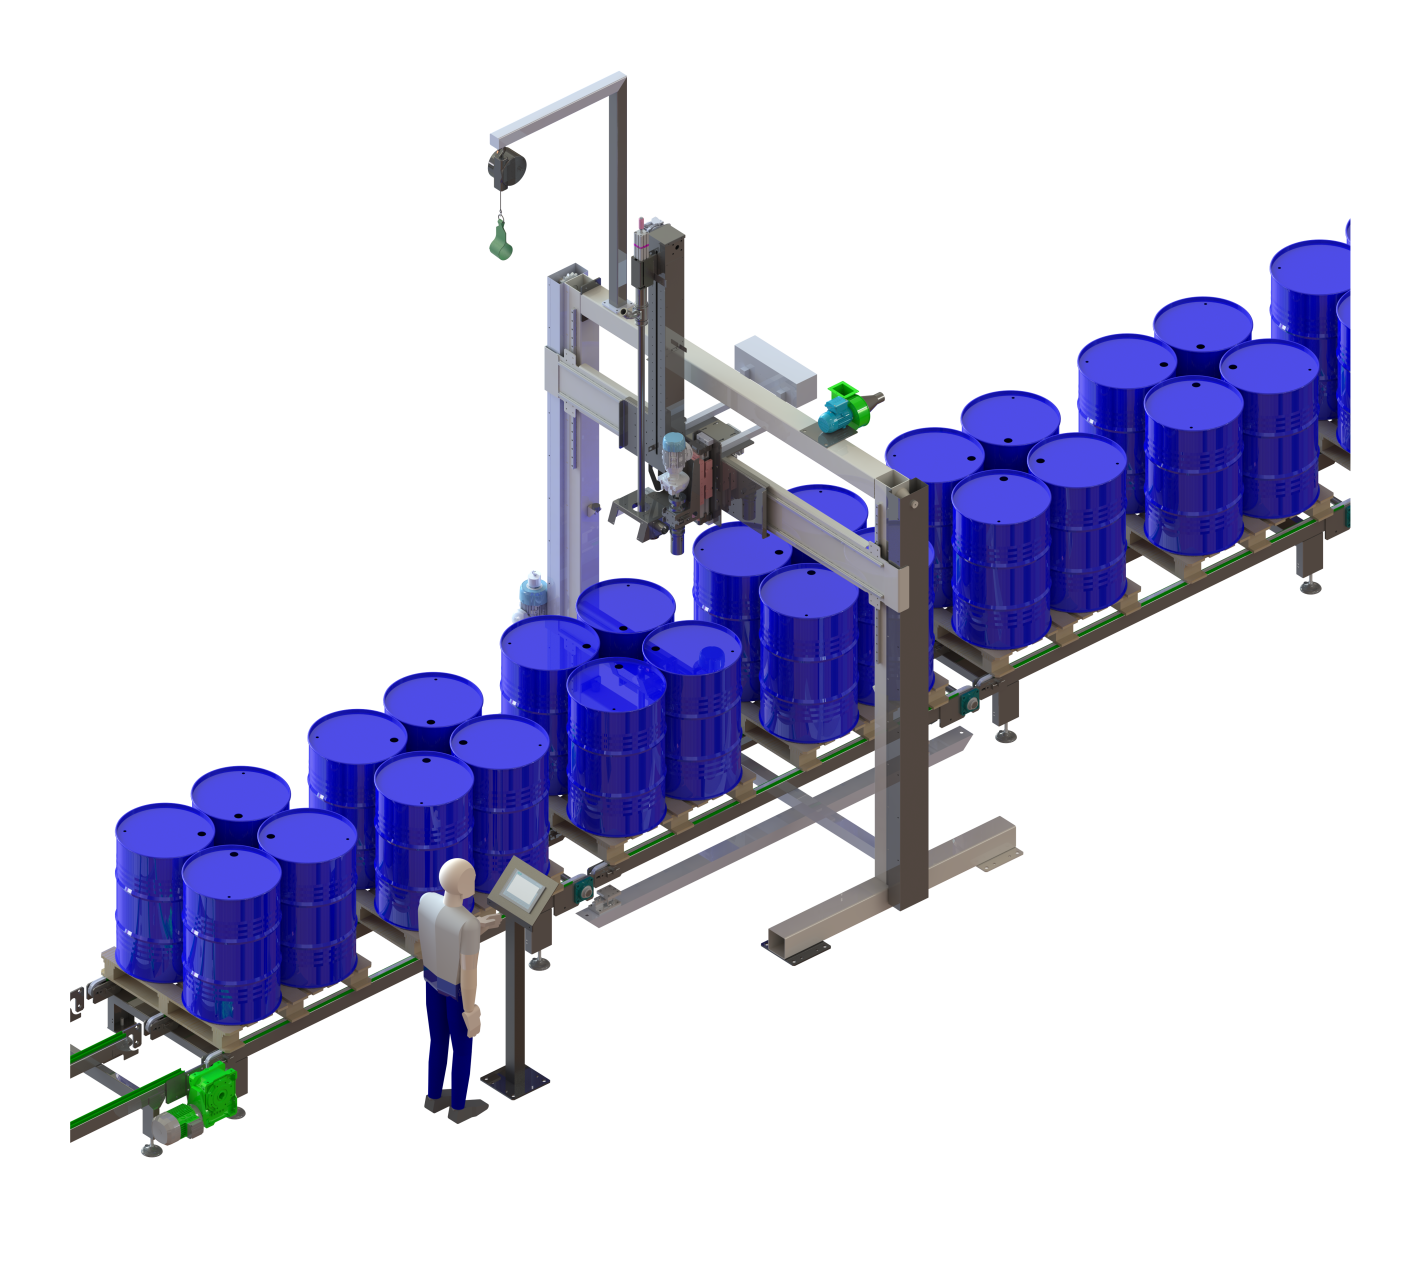
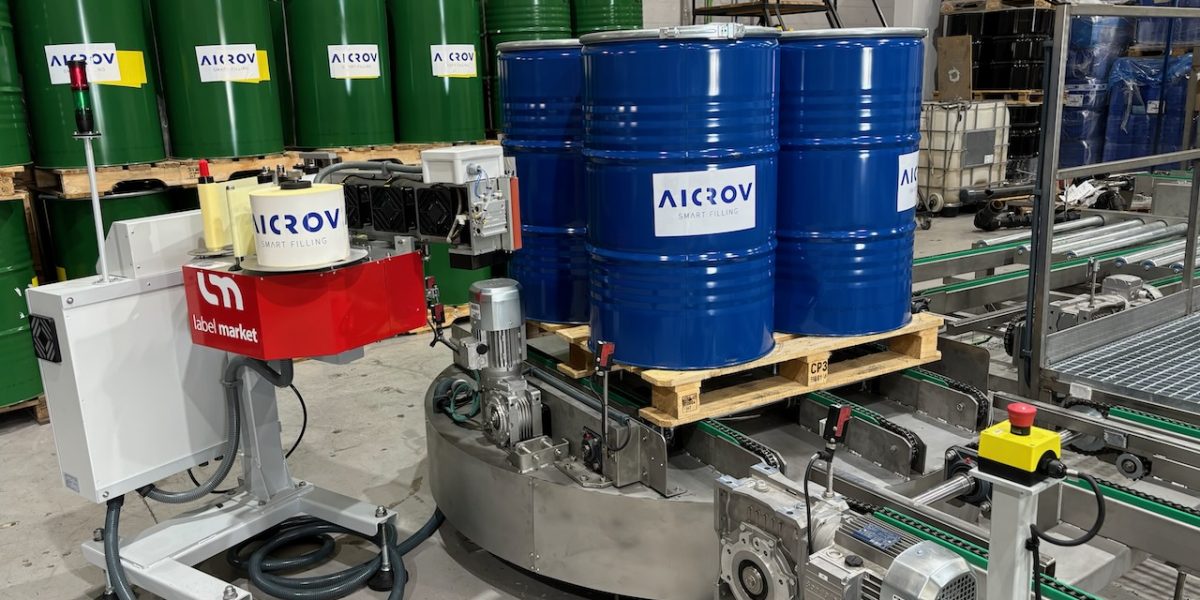
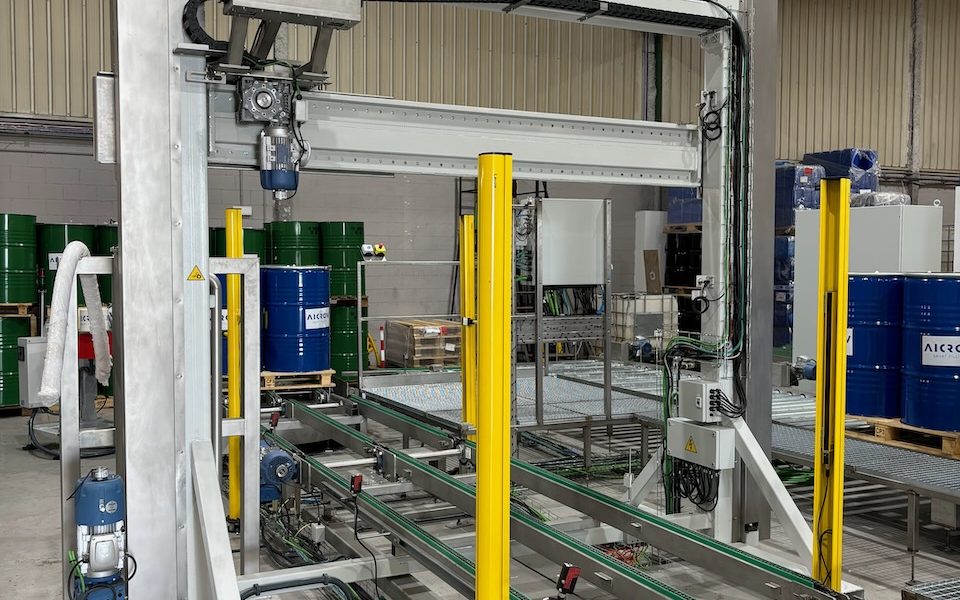
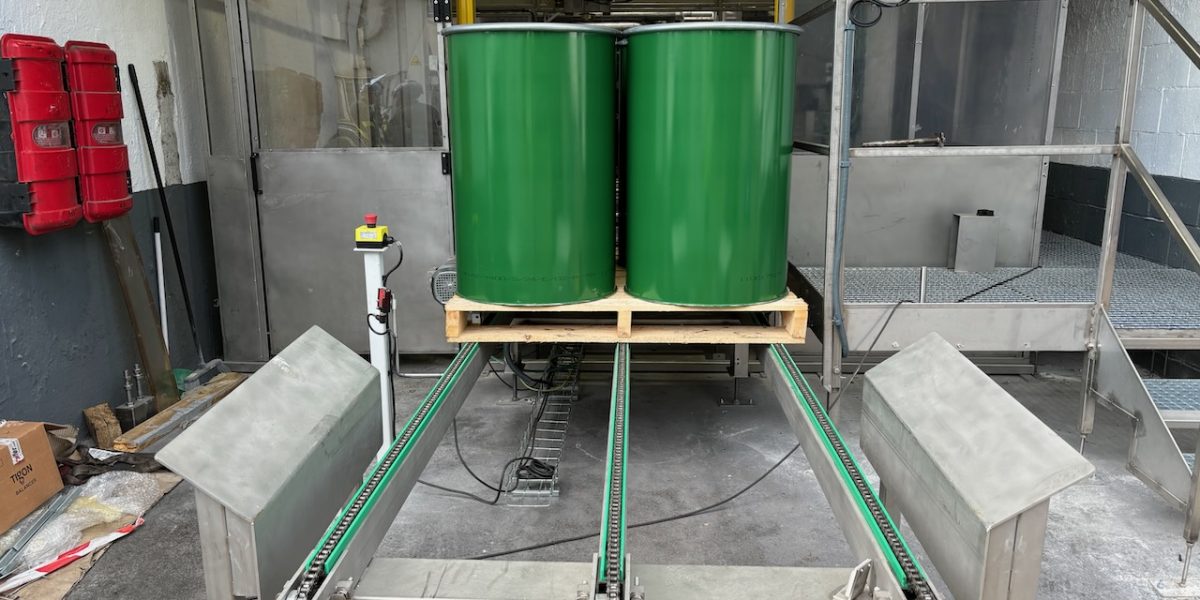
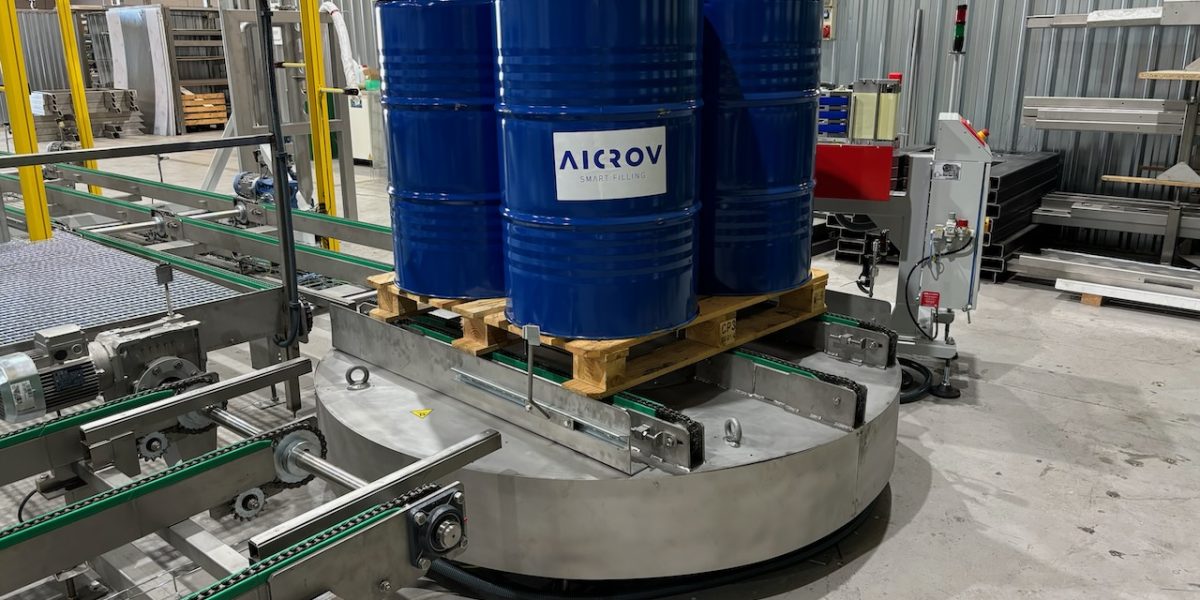
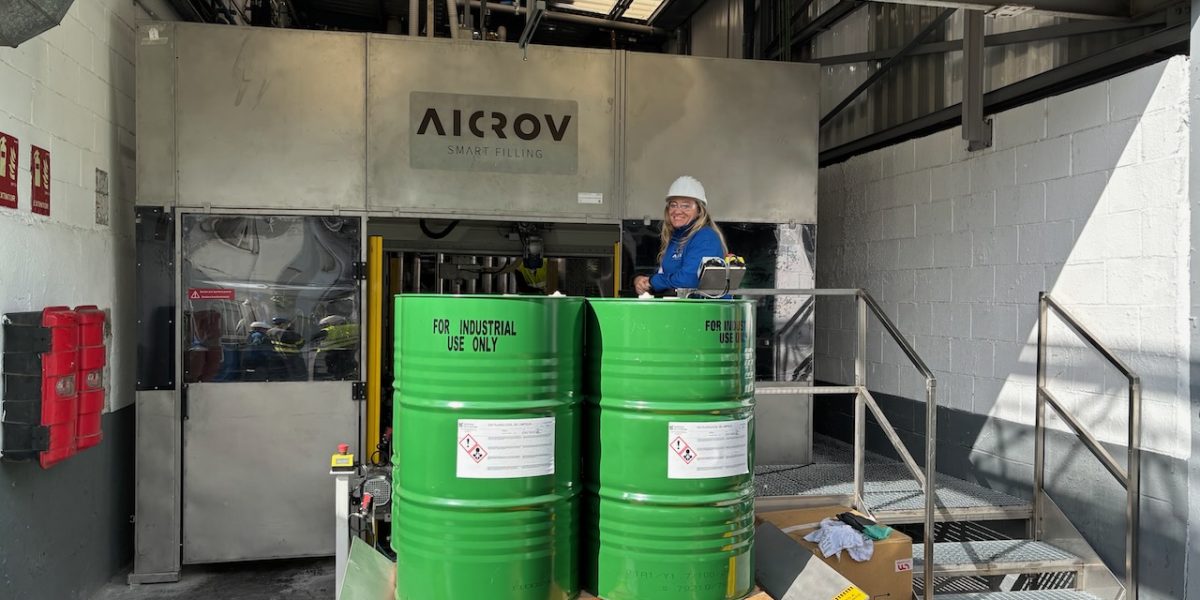
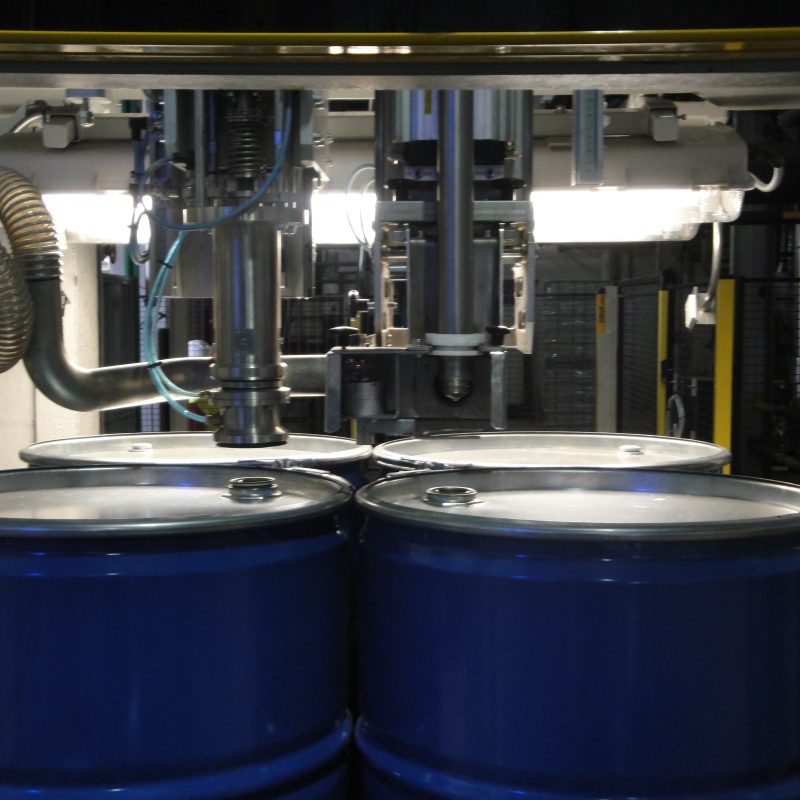
The SP3 fills drums, IBCs and other containers by weight directly on the pallet, from 20 to 1,500 litres, as part of an automatic conveyor line. Once the pallet is in, the operator stays out of the filling area: the machine positions the nozzle over each container, fills it and, depending on the tools fitted, uncaps, caps and seals it.
Advanced series · Automatic · Drums and IBCs on pallet
Main features
- Operator out of the filling area during the whole cycle.
- Bunghole location by joystick teach (standard) or machine vision (option).
- Four-position tool holder: filling, uncapping, capping and sealing on the same head.
- Motorised axes with automatic positioning and working height adjusted to each container.
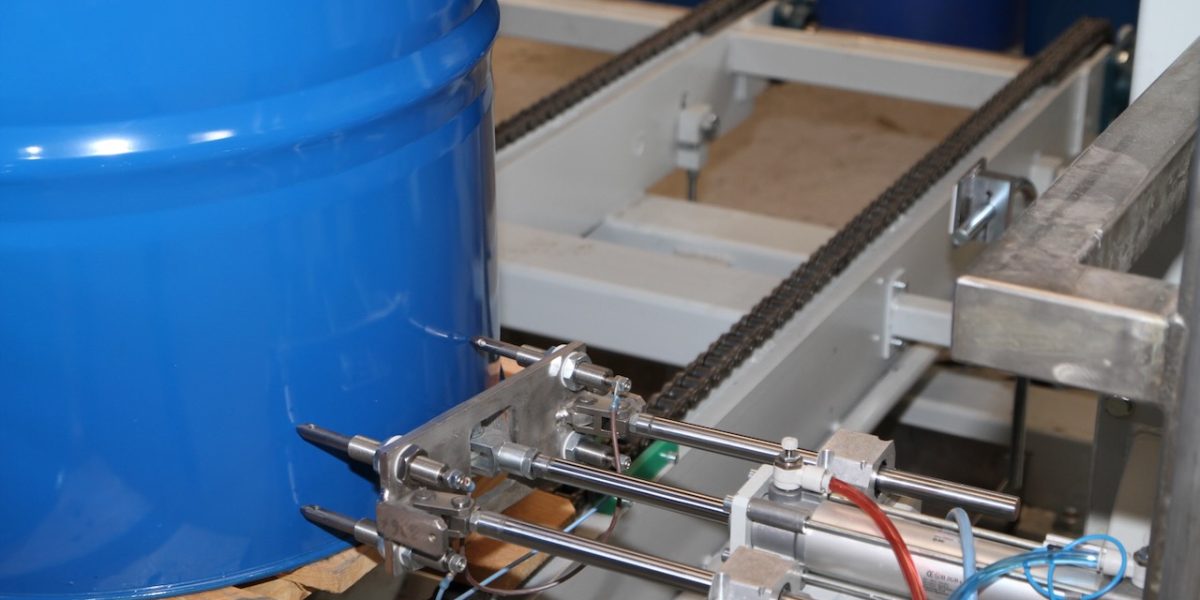
- Weighing conveyor integrated in the control system, with legal-for-trade approvals.
- Control and supervision of the line conveyors and turntables.
- Open industrial components from globally distributed brands, with no proprietary electronics in the control chain: spare parts can be sourced locally.
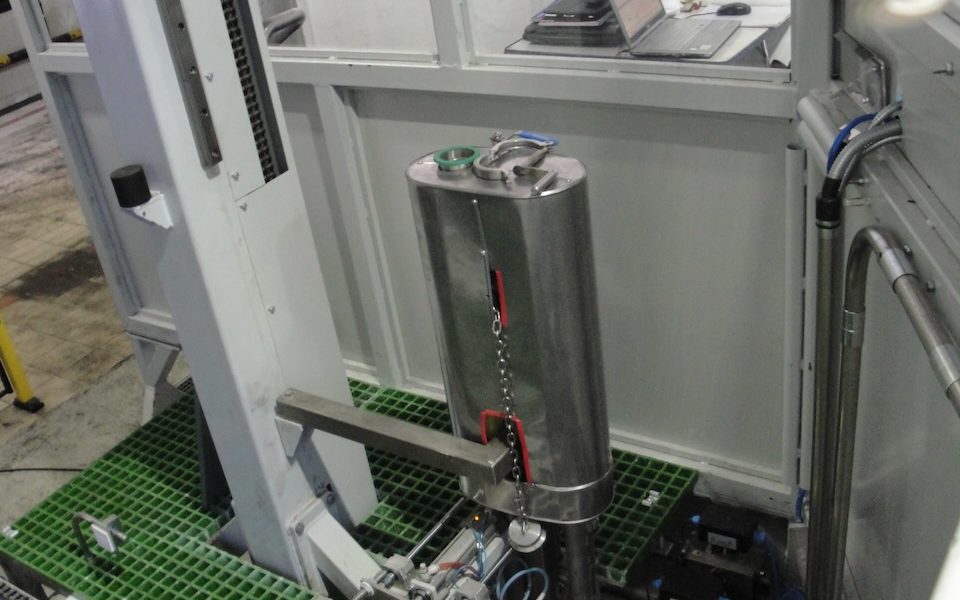
- Interchangeable nozzle, changed quickly and without tools.
- Explosion proof version (ATEX, IECEx) and food-grade version as options.
Technical specifications
| Containers | Drums, IBCs and other containers on pallet, 20 to 1,500 L |
| Output, drums (water-like products) | 60 drums of 200 L per hour filling only · 45 with uncapping and capping · 30 with uncapping, capping and sealing |
| Output, IBCs (water-like products) | 20 IBCs of 1,000 L per hour filling only · 18 with uncapping and capping |
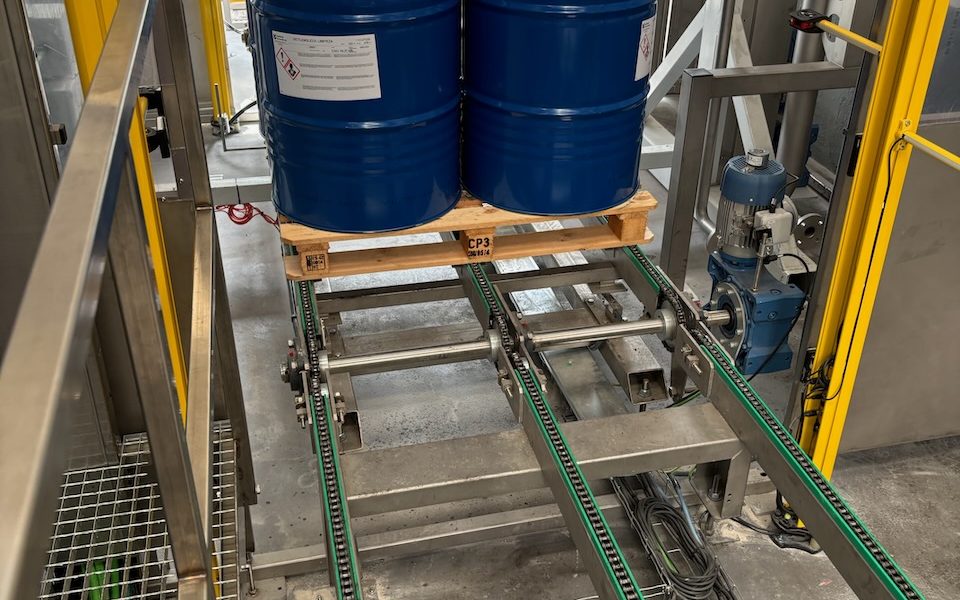
| Weighing | 2,000 mm chain weighing conveyor on four sealed stainless steel load cells, 4,000 kg platform |
| Scale resolution | ±75 g (10,000 divisions), ±125 g (6,000) or ±250 g (3,000) |
| Legal metrology | OIML R76, R51 and R61 (MID), EN 45501, CE-M |
| Bunghole location | Joystick teach (standard) or machine vision (option) |
| Nozzles | More than 80 combinations. AISI 316L as standard; Hastelloy, titanium, PVC, PTFE and other materials on request. Up to 80 °C as standard, up to 210 °C as an option |
| Hazardous areas | Explosion proof version for ATEX, IECEx or the scheme of the country of installation (option) |
| Machine weight | 1,000 to 1,100 kg |
| Utilities | 3 × 380 VAC + N + PE and 6 bar compressed air as standard, adapted to the country of installation |
Tell us about your product and containers
How the SP3 works
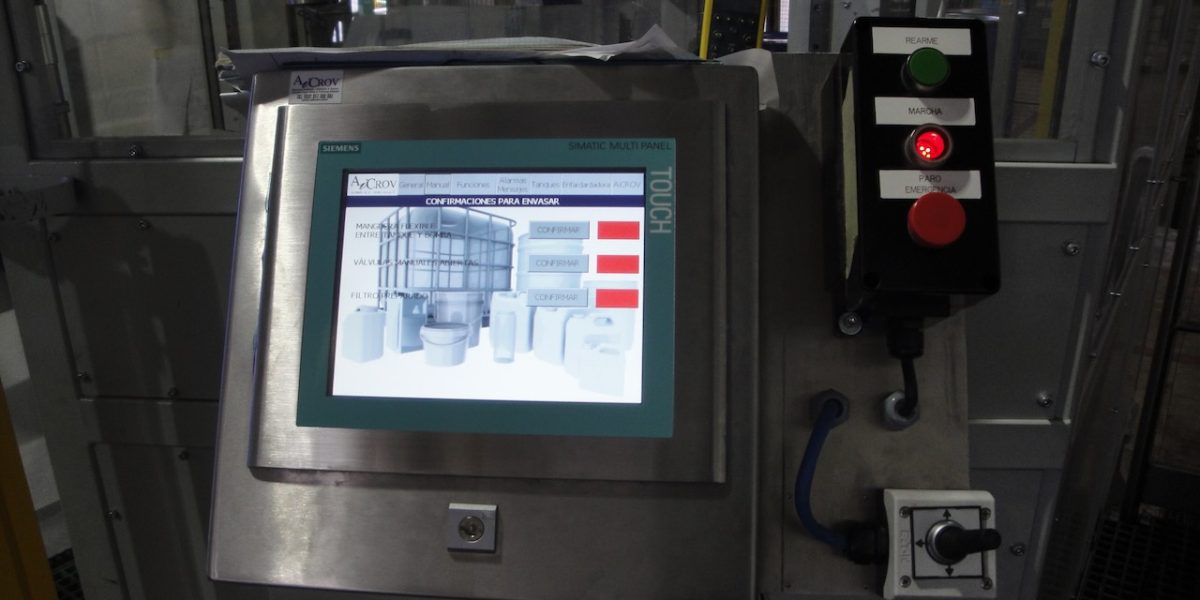
1. The filling recipe and the cycle parameters are selected on the operator panel.
2. Pallets with empty containers are placed on the infeed conveyor.
3. The pallet enters the filling station and stops on the weighing conveyor with repeatable accuracy, with no mechanical stops.
4. The machine locates the container positions: the operator teaches them with the joystick as each pallet enters, or the machine vision system locates them by itself.
5. The head moves over each container, adjusts the working height by motor and performs the operations fitted: uncapping, filling, capping, sealing.
6. When the pallet is complete, it is discharged, the next one enters and the cycle continues.
Teach or machine vision: how bungholes are located
The bunghole is not in the same place on every container: each drum may have been placed turned differently on the pallet. With the standard joystick teach mode, the operator shows the machine the position of each bunghole as the pallet enters, and the machine then runs the whole pallet on its own. With the optional machine vision system, the SP3 takes an image of the pallet, calculates the coordinates of every bunghole and runs the cycle with no operator intervention at all.
Filling control: AiCROVFill®
Every AiCROV machine runs AiCROVFill®, the filling function AiCROV has developed and refined over more than twenty years of installations. The goal is simple: fill each container in the shortest possible time with the accuracy the product requires, and let the customer set the balance between the two.
- Two-speed filling: gross flow for about 95% of the dose, fine flow to finish on target.
- Final weight and top-up: once the nominal net weight is reached the nozzle closes, the settled weight is checked and, if it has fallen below target, the dose is completed.
- Tare control: every pallet entering the scale is compared with its expected weight, so a wrong or already full container is detected before filling.
- Final pallet check: after the last container, the machine compares the pallet’s gross weight with the expected result.
- Flow monitoring: if the flow drops towards zero during filling, the machine stops and raises an alarm.
- Recipes: hundreds of recipes stored per product and container format, named with the customer’s own codes. Changing reference is a selection on the panel, not a readjustment.
Filling modes
Two filling assemblies are available. The structure is in sandblasted AISI 304 stainless steel; the nozzle is AISI 316L as standard, with many other materials available for demanding products.
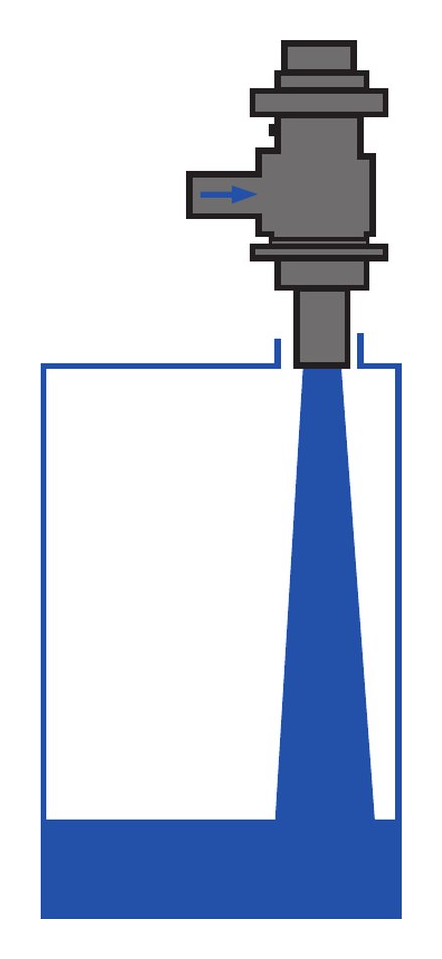
Under bunghole
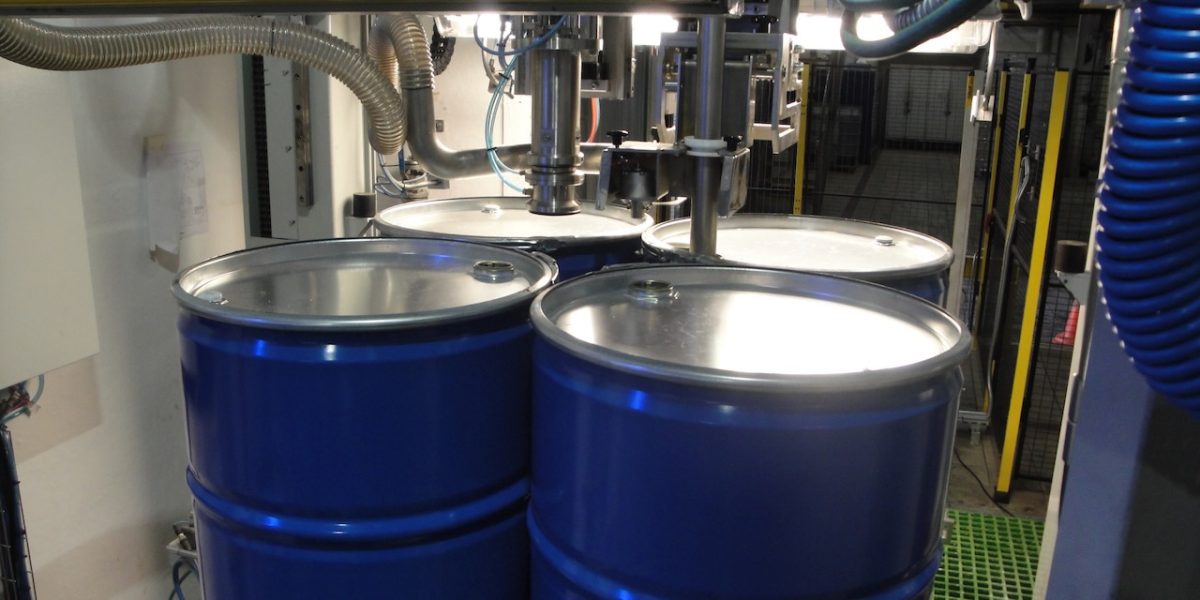
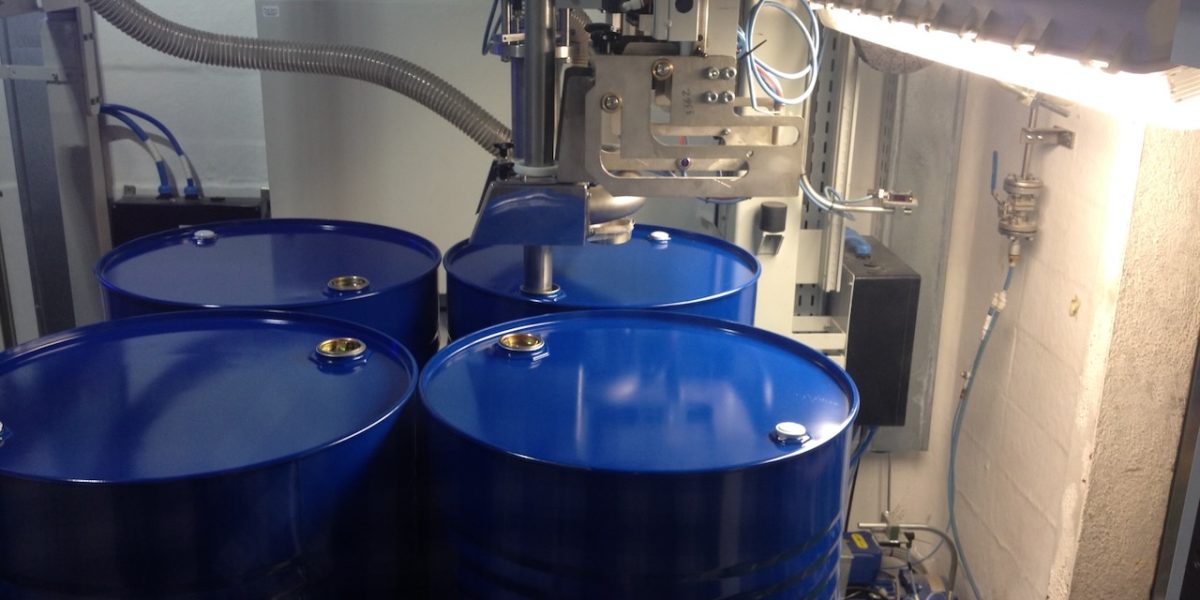
For products that do not foam and are neither flammable nor explosive, including dense and viscous products. The nozzle descends until it is just inside the container and fills from that position.
Immersion filling
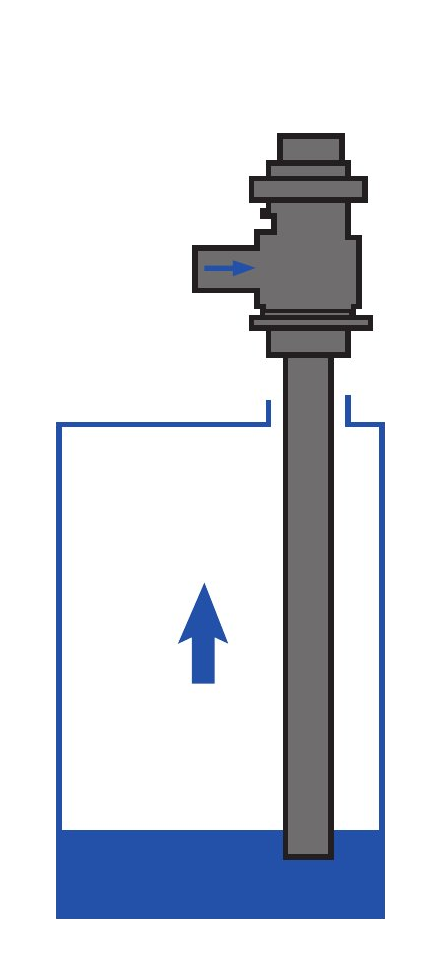
For products that foam, and for flammable or explosive products. The nozzle descends to the bottom of the container and rises slowly, following the product level in real time as the container fills. With the immersion assembly, the filling recipe lets you choose one of three ways of filling:
- From the bottom: the nozzle stays at its lowest programmed position inside the container and performs the whole fill from there. For highly foaming products.
- From the top: the nozzle enters just inside the container and fills from there. For products that do not foam and are neither flammable nor explosive.
- Rising with the product: the nozzle opens at the bottom of the container and rises as it fills. The control system calculates the product height inside the container and keeps the nozzle at that level, stopping at the top of the container, without leaving it, until the fill is complete.
One head, several operations
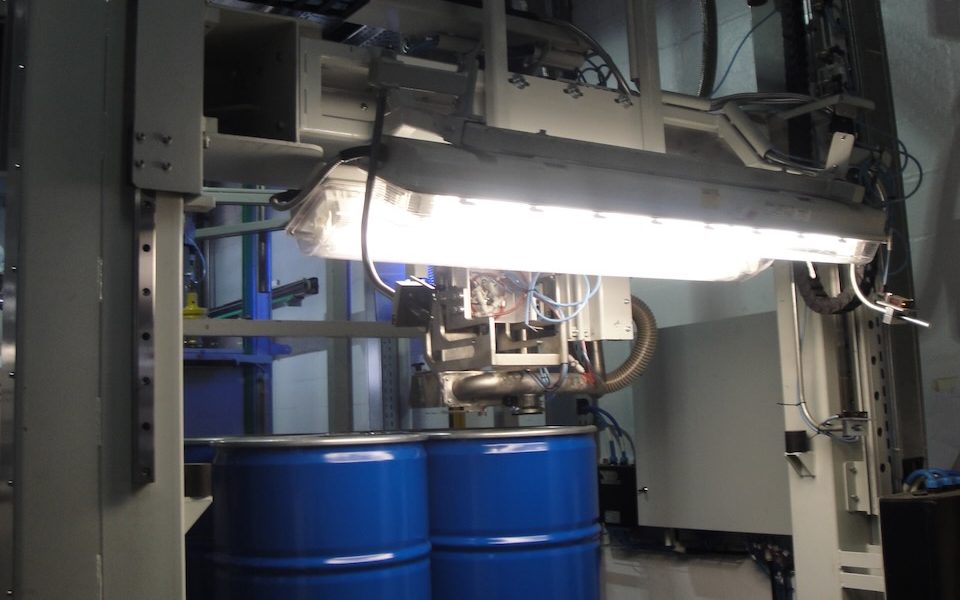
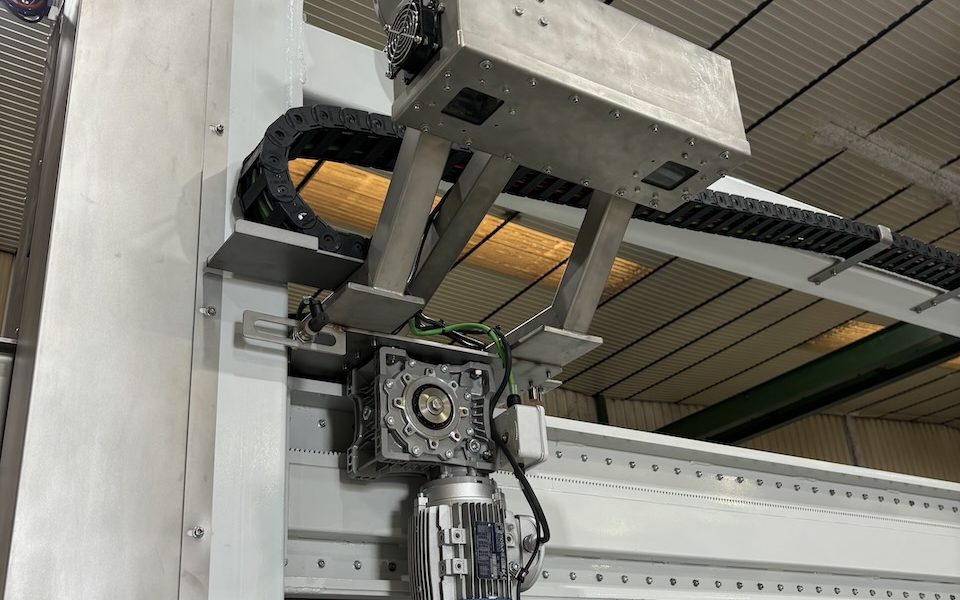
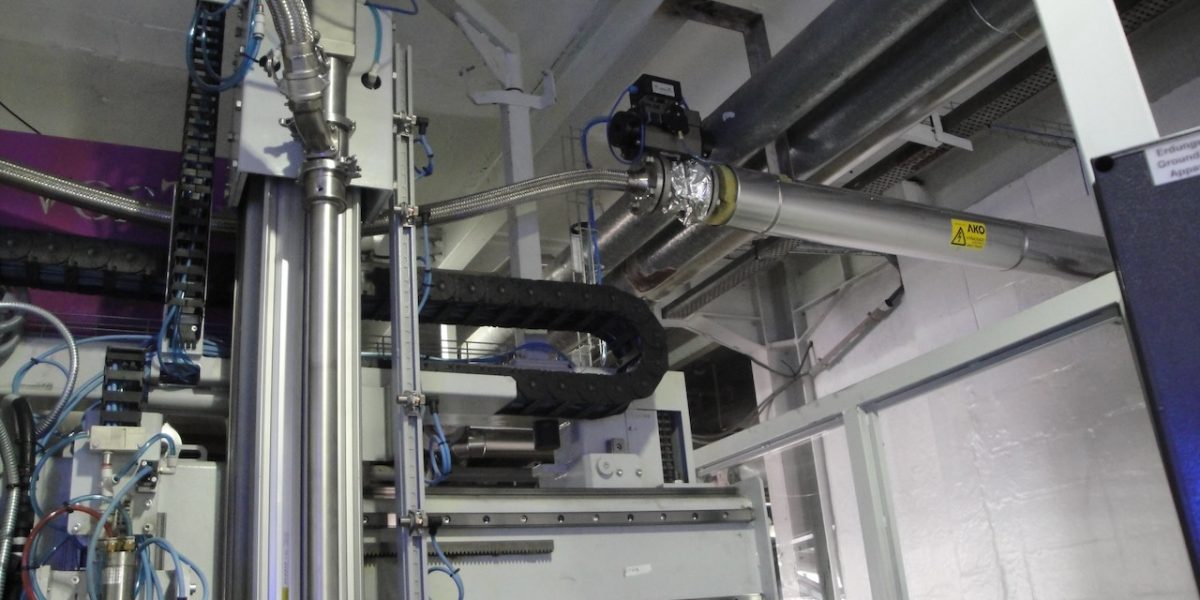
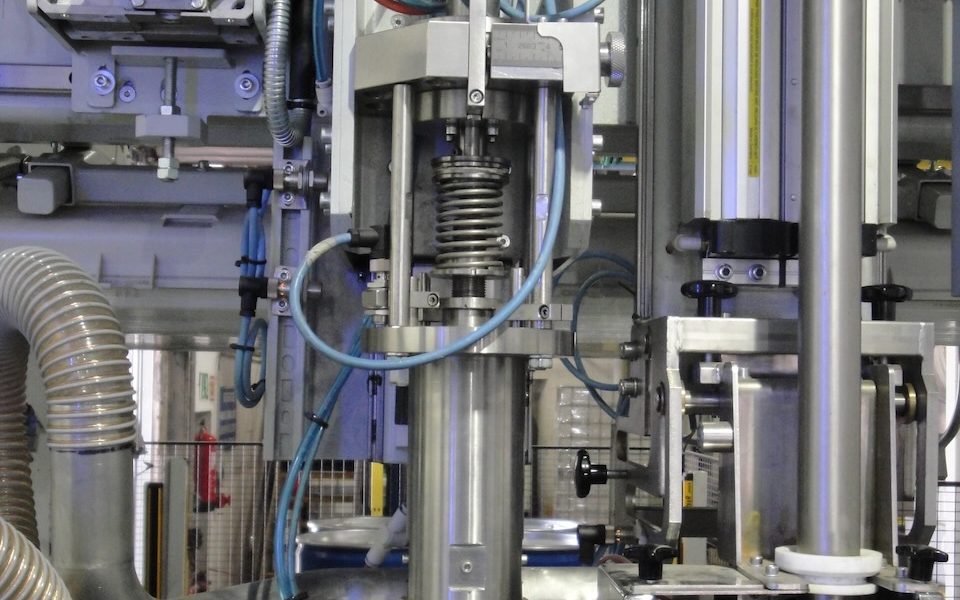
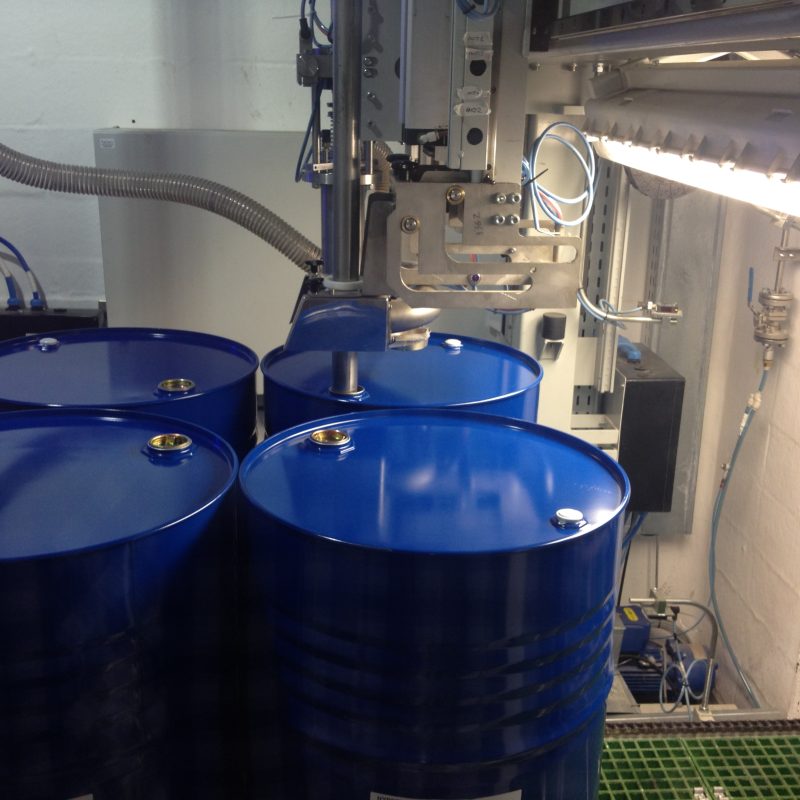
The SP3 is built around a two-axis Cartesian gantry with a four-position tool holder. The usual configuration combines one filling unit with three tools: drum uncapping and capping, IBC uncapping and capping, and drum sealing with metal (Tri-Sure compatible) or plastic seals. The four positions can be combined as the process requires, up to four filling units on the same head, for example to fill different products without changing nozzles. It is the same tool holder and tool set as the Robot Filler: the difference between the two machines is the motion technology, not what they do.
Options
- Machine vision bunghole location
- Nitrogen inerting before, during and after filling
- CIP cleaning of the nozzle
- Product pump control and proportional filling
- Filling records in CSV (date, time, tare, net weight per container)
- Electrostatic grounding control for flammable products
- Overfill detection
- Gas hood and fume extraction
- Nozzle coding
- Closed cabin for hazardous products
- Integration signals with the plant, from simple I/O to full industrial communication
Safety and compliance
The SP3 is designed and manufactured in accordance with European machinery safety legislation, and its documentation is adapted to the regime of the country of installation. The design follows EN ISO 12100 (risk assessment), EN ISO 13849-1 (safety-related control systems), EN 60204-1 (electrical equipment) and EN ISO 13850 (emergency stop), and the risk assessment is carried out on the actual configuration supplied.
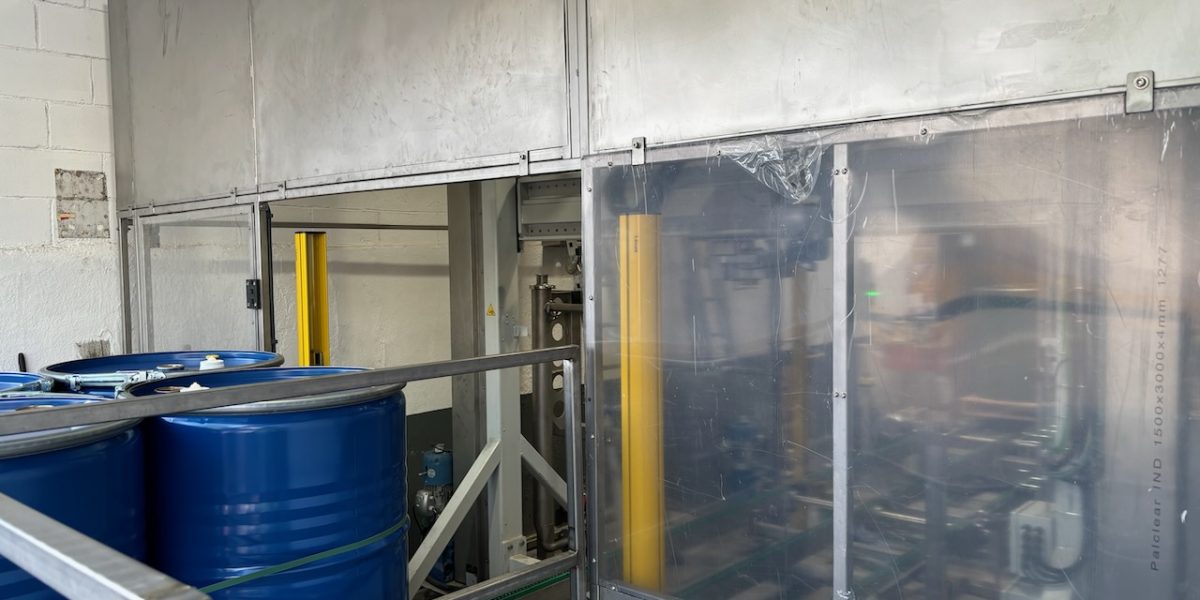
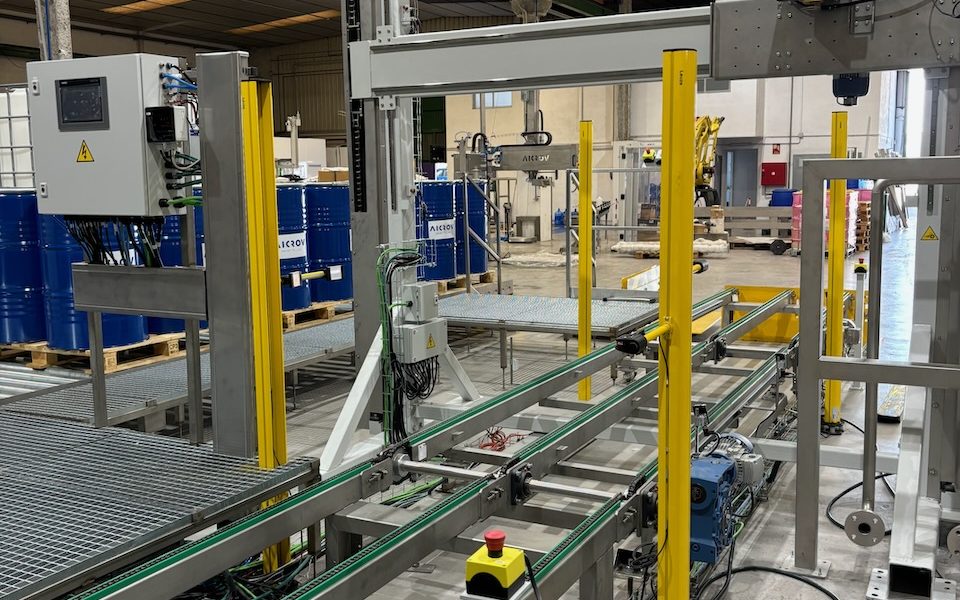
As an automatic machine, the perimeter safety enclosure is part of the supply: interlocked access doors and light curtains with muting at container entry and exit. Emergency stop cuts electrical and pneumatic power, and a loss of air or power leaves the nozzle closed: no spill, no residual movement.
For areas with a risk of explosive atmosphere, the SP3 is supplied in an explosion proof version under ATEX, IECEx or the certification scheme applicable in the country of installation, covering the whole assembly: machine, weighing conveyor, tool holder and tools.
Applications
The SP3 is used wherever drums and IBCs are filled on pallets in volume: chemicals, petrochemicals and lubricants, food (food-grade version as an option) and toll filling and logistics operations. It handles products from water-like to viscous, including foaming, flammable and hot products with the appropriate nozzle and options.
Frequently Asked Questions
What is the difference between the SP3 and the Robot Filler?
They do the same job with the same tools. The SP3 moves the head with a Cartesian gantry; the Robot Filler uses an anthropomorphic robot. The choice depends on the layout, the containers and the plant.
Do I need the machine vision system?
No. In the standard teach mode the operator teaches the bunghole positions once per pallet and the machine does the rest. Machine vision removes that step and makes the cycle fully automatic.
Can the SP3 fill flammable products?
Yes. It is available in an explosion proof version under ATEX, IECEx or the local scheme, with immersion filling, electrostatic grounding control and nitrogen inerting as options.
How accurate is the filling?
Scale resolution goes down to ±75 g, with legal-for-trade approvals (OIML, MID). The final accuracy is set according to the balance between precision and filling rate the product requires.
Can one machine handle different products and container sizes?
Yes. Recipes store the parameters for each product and format, and the nozzle can be changed without tools.
Can the SP3 be integrated into an existing line?
Yes. It is designed to work with conveyors and can exchange signals with the plant, from simple I/O to full industrial communication with filling parameters.
