
SP1 — semi-automatic weigh filling machine for containers on a pallet
Put the pallet on the weighing platform. Align the nozzle with the container. Press start. The machine tares, doses to the net weight and stops. Repeat for every container on the pallet.
That is the whole machine, and it is the point of it. The SP1 is a simple way to stop filling by eye and start filling by weight without unloading the pallet — no conveyors, no plant modification, no line to commission.
Plug & Fill series · Semi-automatic · Containers on pallet

Is this the machine you need?
Yes, if you fill drums, kegs, pails, canisters or IBCs (totes) that arrive and leave on pallets; you fill them a pallet at a time; and an operator is at the filling point anyway.
No, if you handle containers one by one — the LSG, LSB and LSC are simpler and cheaper for that. And no, if you need pallets to move themselves: that is the SP2. If the operator should not have to position the head at all, the SP25. If nobody should be there, the SP3 or the Robot Filler.
Every AiCROV machine handles virtually any industrial liquid — viscous, sticky, foaming, flammable, corrosive. What changes with the product is the nozzle, the materials in contact with it and how the dose is controlled. Not the model.
What decides the model is the container format, the throughput you need, and how much of the handling you want the machine to do. That is why our range is not organized by industry. A detergent plant and a lubricants plant filling the same drum at the same rate buy the same machine.
How it works
1. Filling recipe and net weight are selected on the operator panel.
2. Filling height is adjusted to the container format, without tools.
3. The pallet of empty containers is placed on the weighing platform.
4. The operator presses the release button and moves the filling head until the nozzle is over the container opening. On releasing the button, the head locks in place.
5. On start, the system tares automatically and fills to the net weight.
6. Alignment and filling repeat for each container on the pallet.
7. The full pallet is removed and a new cycle begins.

SP1 Gravimetric Filling Machine — Dual Scale, Explosion Proof | Syngenta, Colombia | AiCROV
An SP1 with an additional scale for Syngenta in Colombia, in an explosion proof version: one machine fills the containers on the pallet and the smaller containers on the second scale.
More videos of this machine
Other installations and configurations, filmed in our workshop and at customer sites.

Semi-Automatic Drum & IBC Filling Machine SP1 — Weight Filling on Pallet | Chemical | AiCROV

SP1 Gravimetric Filling Machine — Dual Scale, Drums to Jerrycans | Food, USA | AiCROV

SP1 Liquid Filling Machine + Two Scales + Gas Hood

SP1 Automatic Filling Machine — 20 L Jerrycans on Pallet | Peracetic Acid | AiCROV

SP1 CL with Mobility Base

SP1 with Canister Scale: How to Create a New Container Recipe
Filling modes: two assemblies
Two filling assemblies are available, and the choice is made when the machine is ordered: the assembly is a physical part of the machine, not a setting. Both are made of sandblasted AISI 304 stainless steel; the nozzle is AISI 316L as standard, with other materials available for demanding products.
Under bunghole filling
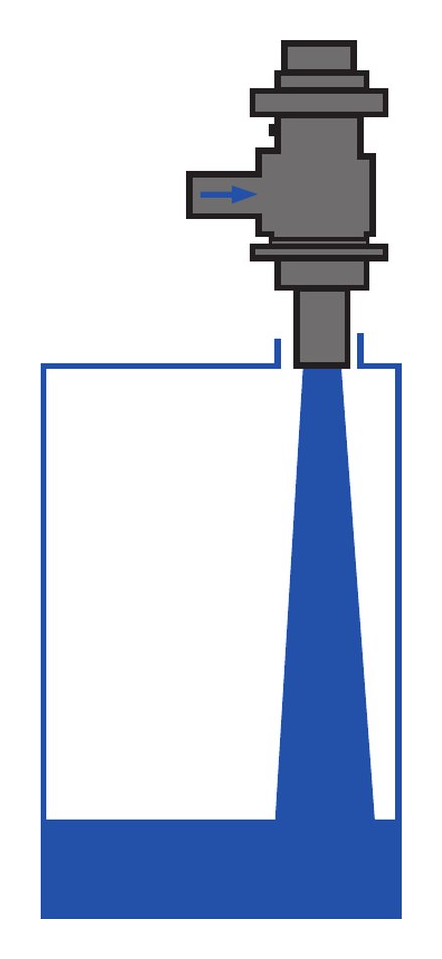
Normally used for products that do not foam and are neither flammable nor explosive, including dense and viscous products. The nozzle descends until it is just inside the container and fills from that position. This assembly fills under the bunghole only.
Immersion filling

Normally used for foaming products, and for flammable or explosive products. The nozzle descends to the bottom of the container, and the filling recipe chooses one of three ways of filling:
- Rising with the product: the nozzle opens at the bottom and rises as the container fills. The control calculates the product height inside the container and keeps the nozzle at that level, stopping at the top of the container, without leaving it, until the fill is complete.
- From the bottom: the nozzle stays at its lowest position for the whole fill. For extremely foaming products.
- Under bunghole: the nozzle enters just past the bunghole and fills from there, as the under-bunghole assembly does.
If your range includes foaming or flammable products, or may include them later, choose the immersion assembly: it covers every way of filling.
Machine architecture
A self-supporting structure carries a vertical column on which the filling head travels, housing the dosing group and its actuation. The weighing platform sits beneath the whole pallet, and its weighing terminal is integrated into the control system — weight governs the cycle directly, not through an external indicator reporting to a separate PLC.
The control cabinet and the pneumatic group complete the assembly.
Two versions: SP1 and SP1 two-axis
In the standard SP1 one axis pivots and the other is linear, so moving from one bunghole to the next means adjusting both axes and aiming again. In the two-axis version the axes are independent: X and Y move separately.
That matters when the pallet carries small containers in a grid — canisters of 20, 30 or 60 litres arranged 3 × 3, 4 × 4 or 3 × 4. Once the operator is lined up on a row or a column, filling the rest of that row means moving one axis only. When the row is finished, they move to the next one and again move a single axis.
For drums and IBCs, where there are few containers per pallet, the standard version is enough. For pallets of small containers the two-axis version is markedly easier for the operator, and over a full shift it means many more containers filled.

SP1 2-Axis (X–Y) Semi-Automatic Filler — Drums, IBCs, Jerrycans, Pails | AiCROV
Inert gas filling (optional)
Any AiCROV machine can be supplied to fill under an inert atmosphere. It is fitted as an accessory, and it touches the nozzle, the control cabinet and the recipe.
How it is built. The nozzle carries a small passage through which the gas flows. A dedicated solenoid valve in the main control cabinet drives that flow, so the gas is part of the filling cycle rather than something an operator does alongside it.
When the gas flows is a recipe parameter, not a fixed setting. You choose to inert before the nozzle opens, during filling, after the target weight is reached, or any combination of the three — and you set how many seconds each phase lasts. Different products need different answers, and the machine stores one per product.
Why a small amount of gas is enough. Nitrogen is heavier than air. A short burst into the bottom of an empty container leaves a layer of nitrogen sitting there, and filling then begins inside that atmosphere rather than in air. As the product level rises, the nitrogen is pushed up ahead of it and stays between the liquid and the container opening. A little more at the end, before the container is capped, and the product has never touched air.
It is not always nitrogen. The gas is chosen for the product; nitrogen is simply the most common.
Inerting by overpressure is the other route: capping assemblies that pressurize the inside of the container to a few millibars immediately before the cap goes on.
And the case that is not about product quality at all. Filling a flammable product into a metal container can generate a spark as the liquid starts to flow. Displace the oxygen first and there is nothing to ignite. On some installations that is the whole reason the inerting is there.
The nozzle is interchangeable. It can be replaced by a different model or diameter without modifying the structure or the filling head, which means the machine can be adapted to a different product or a different container years after it was bought. How nozzles are cleaned →
AiCROVFill®
Weighing a container while you fill it is not difficult. Getting the last hundred grams right, every time, on a product that foams, settles or clings to the lance, is the whole job. AiCROVFill® is the filling control AiCROV has developed and refined since its first filling machine in 2009, installation after installation.
A software ecosystem, not a single function. AiCROVFill® is the whole of AiCROV’s filling software, built around one aim: to fill as accurately and as fast as the product allows — efficient in time, effective in the result — and always safely.
Misalignment control. If the nozzle meets resistance as it descends into the container, it returns to its upper position and waits for the operator to realign it. It does not force the container.
Final weight control and top-up. Once the nominal net weight is reached, the nozzle closes. For a set interval afterwards the system keeps watching the settled weight, and if it has fallen below the nominal value it reopens and completes the dose — as many times as needed. This is the difference between a container that reads correct at the moment of closing and one that reads correct on the customer’s scale.
Compensation for the submerged lance. In immersion filling the nozzle can stay below the product surface — because the operator has set it to fill under the level to keep a foaming product quiet, or because, near the top of a full container, it cannot rise any further without leaving the opening. A submerged lance displaces its own volume of product, and the scale reads that displacement as weight. Close the nozzle at the nominal value, draw the lance out, and the container is suddenly tens or hundreds of grams short — a fill that looked perfect now fails the tolerance. AiCROVFill® knows where the lance is: its position is controlled, so the volume it occupies inside the product is known at every moment. The control calculates the weight that volume accounts for and doses exactly that much more before closing, so the net weight is right after the lance comes out, not only while it is still in.
Automatic compensation of the product still falling after the valve closes. When the valve closes, some product is still on its way into the container. How much depends on the machine, and on conditions outside it: supply pressure, flow rate, product temperature and viscosity. If the recipe carries a fixed value for that product, AiCROVFill® uses it. If that value is set to zero, the machine learns it: container after container it measures the result and moves the cut-off point by itself, so the batch settles on the nominal weight and stays there as conditions drift.
Recipe-based operation. Filling parameters are stored per product and per container format. Changing reference is a selection on the panel, not a readjustment of the machine.
Built from parts you can buy yourself
This machine is built with industrial components from globally distributed brands — control, pneumatics, sensors and weighing elements — with no proprietary electronics or firmware anywhere in the control chain.
This matters on the day something fails. You source the spare part yourself, in your own market, at market price. Your maintenance staff work on platforms they already know. You do not wait for a shipment from Tarragona to replace a component that is on a shelf twenty minutes from your plant.
It is a deliberate design decision, and we think a machine that holds your plant hostage is not a machine you should buy.
Safety and compliance
The machine is designed and manufactured in Europe, to European machinery safety legislation, and carries the CE marking. That is our starting point for every market we ship to. Outside the EU, most markets mirror that legislation through a transposition or an equivalent framework of essential health and safety requirements, so AiCROV starts from the same design and the same risk assessment everywhere, and adapts the marking, the declaration and the documentation to the regime of the country of installation.
The design follows the harmonised framework customary in the sector: risk assessment and risk reduction to EN ISO 12100, safety-related parts of control systems to EN ISO 13849-1, electrical equipment to EN 60204-1, emergency stop to EN ISO 13850.
The risk assessment is carried out on the configuration actually supplied, not on a generic model, and the resulting measures are built into the mechanical design, the electrical design and the control software.
- Emergency stop — cuts power and pneumatic pressure to the actuators simultaneously. Reset is manual and deliberate.
- Head braked by default — the filling head stays locked except while the operator holds the release control. It cannot drift during filling.
- Passive nozzle lock — without pneumatic pressure the nozzle cannot open.
- Safe behaviour on failure — no residual head movement, no product flow.
Every AiCROV machine can be supplied in an explosion proof version. Where the machine is going into an area with a risk of explosive atmosphere, that protection is engineered as a specific part of the project, under the certification scheme that applies in the country of installation — ATEX in Europe, IECEx in many other markets, NEC in the United States. Explosion proof versions are designed for Zone 1 or Zone 2 hazardous areas, or the equivalent Class I, Division 1 or 2 under NEC, depending on the project.
This is not a variant we assemble occasionally. Most of the explosion proof machines AiCROV has installed are in plants that also run standard machines from us — the same customer, two versions, depending on which room the machine stands in.
Explosion proof filling machines →
Connection parameters — voltage, frequency, neutral and earthing arrangement, electrical and compressed air connection types — and the operator panel language are defined with you during order engineering, in accordance with the regulations and the usual practice of the country of installation. The starting point is always the CE-compliant design; the local requirements are built in from the start of the order, not retrofitted afterwards.
Technical specifications
| Type | Semi-automatic, weigh (gravimetric) filling |
| Series | Plug & Fill |
| Containers | Drums, kegs, pails, canisters and IBCs, on a pallet, 20 to 1,500 litres (5 to 400 gal); from 0.2 L with an additional scale |
| Throughput | 80 to 130 canisters/hour (20 L), depending on configuration · 65 drums/hour (220 L) · 15 IBC/hour (1,200 L) |
| Filling accuracy | ±0.1% of the nominal fill (to be confirmed for each case) |
| Weight scale resolution | ± 50 g |
| Inert gas filling | Available as an accessory |
| Filling assembly | Under bunghole, or immersion (the immersion assembly also fills under bunghole or from the bottom, selected by recipe) |
| Height adjustment | 550 mm, servo |
| Pump control | 3 potential-free contacts for an on-site pump or a coarse/fine pilot valve |
| Power | 240 V, 50–60 Hz, <1 kW |
| Air pressure | 6 bar (other pressures on request) |
| Working temperature | −10 °C to +45 °C |
| Product temperature | 0 °C to +130 °C |
| Product connection | 1½” male camlock |
| Weight | 700 kg |
| Explosion proof version | Available |
| Installation | Plug & Fill — no plant modification, no conveyors |
Filling throughput is set by the product and the container, not by the model: when they only fill, the SP1, SP2, SP25, SP3 and Robot Filler reach the same cadence, around 60–65 drums per hour. What changes between models is the level of automation. When the machine also uncaps and caps the container, as the SP3 and the Robot Filler can, the cadence is lower.
Frequently Asked Questions
Can the SP1 fill IBCs?
Yes. It fills any container that travels on a pallet, from small canisters up to IBCs, with the filling height adjusted tool-free and the nozzle chosen for the product and the opening.
How accurate is it?
The weighing platform resolves to ±50 grams, weighing the whole pallet. Accuracy is held after closing: AiCROVFill® re-checks the settled weight and tops up if the product has settled.
Does it need an operator?
Yes. The SP1 is semi-automatic: the operator aligns the nozzle with each container and starts the cycle. Taring, dosing and dose control are automatic.
Do I need to modify my plant to install it?
No. Power, compressed air and product supply. No conveyors, no foundations, no line integration.
Can I change what the machine fills later on?
Yes. The nozzle is interchangeable without modifying the structure or the head, and filling parameters are stored per product and container as recipes.
Can it fill flammable products?
Yes, in an explosion proof version engineered for the certification scheme of the country of installation. Flammable products are normally filled with the immersion assembly, which keeps the nozzle below the product level, and electrostatic grounding control is available as an option.
What is the difference between the SP1, the SP2 and the SP25?
The SP1 is the pallet on a platform with the head moved by hand. The SP2 adds automatic pallet movement by conveyors. The SP25 motorises the head on all three axes and can go up to fully automatic with machine vision.
Not sure this is the right machine?
Tell us what you fill, into what container, and how many per hour. We will tell you which model fits — and we will tell you when none of ours does.
Related projects
Real installations of our filling machines in different industries.

SP1 with two scales and a gas extraction hood for aggressive products — Bulgaria
A chemicals producer in Bulgaria needed to fill aggressive products into containers on pallets without stopping between containers and without exposing the operator to fumes.

SP1 in its two-axis version for adhesives and greases, faster on containers arranged in rows — Belgium
A producer of adhesives and greases in Belgium fills many small containers set out in rows on the pallet, as well as drums and IBCs.

One SP1 with dual scale for every container, from 10 L jerrycans to 1,000 L IBCs — food producer, USA
A US food producer wanted a single machine for every container in the plant, from 10-litre jerrycans to IBCs.

SP1 with a custom gas extraction hood for corrosive fluorine derivatives — drums and IBCs, Italy
One of Europe’s largest producers of fluorine derivatives needed to fill drums and IBCs with products that give off corrosive gases.

SP1 and LSG for Lubricants — Drums, IBCs and Jerrycans for TotalEnergies Belgium
TotalEnergies Belgium needed to fill lubricants into every container size, from small jerrycans to IBCs, with legal-for-trade weighing and few operators.

Three SP1 Fillers with Dual Scale, from 25 L Jerrycans to 1,000 L IBCs — Syngenta, Colombia
Syngenta wanted one machine for very different containers, from 25-litre jerrycans to 1,000-litre IBCs, and some of its products are flammable.

SP1 with an extra scale for detergents and cleaning products, from 1 L bottles to IBCs — Serbia
A Serbian manufacturer with seventy years of history needed to fill detergents and cleaning products, which foam, into containers from 1-litre bottles to IBCs.

SP1 semi-automatic weight filler for drums, IBCs and jerrycans on the pallet — Budenheim, Spain
Budenheim needed to fill liquid and viscous products into many container types on pallets, without a fixed installation and starting production straight away.

SP1 filling peracetic acid into 20 L jerrycans on the pallet — PeroxyChem (now Evonik), Spain
PeroxyChem needed to fill peracetic acid, an aggressive and oxidizing product, into 20-litre jerrycans already on the pallet, safely for the operator.

Tell us about your product and containers
We will contact you